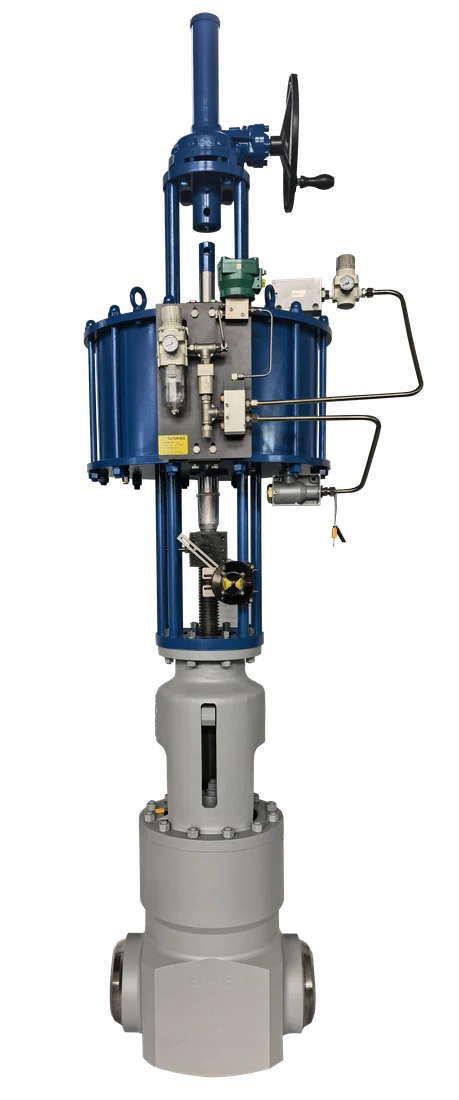
Dervos valve · Product specification
Forged Gate Valve
Gate valve with the pressure boundary formed from a single forged billet. Chosen where thermal cycling or wall thickness makes casting soundness the risk.
- Size
- NPS 2 - 24 (DN 50-600)
- Pressure class
- Class 900 - 4500
- Body material
- A105, A182 F11, F22, F91, F92, WB36, F347
- End connection
- BW to ASME B16.25, SW, flanged RTJ
Catalogue ranges for initial selection. Final rating and configuration are confirmed against your project specification.
Have an MTO or datasheet? Send it with size, class, material, quantity and required delivery.
01 / Selection data
Technical specifications
Use these ranges to shortlist the valve. Values marked “confirm per order” depend on the selected size, material or project standard.
Swipe or scroll sideways to view the full table.
| Parameter | Specification | Basis |
|---|---|---|
| Size | NPS 2 - 24 (DN 50-600)The maximum forged size is confirmed per item against press and handling capacity. | Catalogue range |
| Pressure class | Class 900 - 4500 | Catalogue range |
| Design temperature | up to 650 °C / 1200 °FSet by the body grade and the ASME B16.34 rating table. | Configuration dependent |
| Body construction | One-piece integral forged pressure boundaryWe state per size which features are integral to the forging and which are welded. | Catalogue range |
| Bonnet | Self-energising pressure seal | Catalogue range |
| Medium | Superheated steam, feedwater, hydrogen, process gas | Catalogue range |
| Body material | A105, A182 F11, F22, F91, F92, WB36, F347 | Catalogue range |
| Trim material | F6a / F6NM, Stellite 6 hardfaced | Catalogue range |
| Wedge | Flexible wedge, solid wedge on request | Catalogue range |
| End connection | BW to ASME B16.25, SW, flanged RTJButt weld is the normal choice; flanges are unusual at these classes and need justification. | Catalogue range |
02 / Engineering
Valve design & materials
One-piece forged pressure boundary
Body and neck from a single billet with the internal form machined out, not a body welded to a forged neck and not forged ends welded to a cast centre.
No body weld to examine
Nothing through the pressure boundary to radiograph, heat treat and re-radiograph over the life of the valve. If a body weld appears on the ITP, you are not buying this.
Worked grain flow
Forging orients the grain with the section instead of leaving the as-solidified structure, which improves through-thickness properties where the crotch sees the steepest thermal gradient.
One body, one heat number
Carried from the mill certificate through machining to the nameplate and confirmed by PMI, rather than inferred from a batch.
Pressure seal bonnet
Standard at these classes. Line pressure energises the joint, so no bolt preload to lose through thermal cycling.
Reference material configurations
Material combinations are examples for selection; the final bill of materials is agreed for each order.
Swipe or scroll sideways to view the full table.
| Part | Carbon steel | Alloy steel | F91 / F92 |
|---|---|---|---|
| Body | A105 / A105N | A182 F11, F22 | A182 F91, F92 |
| Seat ring | 13Cr + Stellite 6 | 13Cr + Stellite 6 | F91 + Stellite 6 |
| Wedge (flexible) | A105 + Stellite 6 | F11 / F22 + Stellite 6 | F91 + Stellite 6 |
| Stem | A182 F6a | A182 F6a Cl.2 | A182 F6NM / 422SS |
| Bonnet | A105 / A105N | A182 F11, F22 | A182 F91, F92 |
| Pressure seal ring | Flexible graphite + SS liner | Flexible graphite + SS liner | Flexible graphite + Inconel liner |
| Thrust ring (segmental) | A105 | A182 F11 / F22 | A182 F91 |
| Retainer segments | A105 | A182 F11 / F22 | A182 F91 |
| Gland | A105 | A182 F11 / F22 | A182 F91 |
| Gland flange | A105 | A105 | A182 F91 |
| Stem packing | Flexible graphite | Flexible graphite | Flexible graphite, low-leakage set |
| Gland eyebolt / pin | A193 B7 / A194 2H | A193 B16 | A193 B16 |
| Yoke | A105 / WCB | A105 / WCB | A105 / WCB |
| Yoke bushing | Ni-Al bronze | Ni-Al bronze | Ni-Al bronze |
| Back seat | 13Cr overlay | 13Cr overlay | Stellite overlay |
| Handwheel | Ductile iron / carbon steel | Ductile iron / carbon steel | Ductile iron / carbon steel |
| Nameplate | AISI 304 | AISI 304 | AISI 304 |
03 / Reference dimensions
Dimensions & approximate weight
Typical reference values only. Request the approved GA drawing and confirmed weight for your selected class and configuration.
Swipe or scroll sideways to view the full table.
| NPS | DN | Face to face / end to end | Approx. weight |
|---|---|---|---|
| NPS 2 | DN 50 | 368 mm | ~55 kg |
| NPS 3 | DN 80 | 470 mm | ~105 kg |
| NPS 4 | DN 100 | 546 mm | ~180 kg |
| NPS 6 | DN 150 | 705 mm | ~390 kg |
| NPS 8 | DN 200 | 832 mm | ~700 kg |
| NPS 10 | DN 250 | 991 mm | ~1150 kg |
| NPS 12 | DN 300 | 1130 mm | ~1750 kg |
| NPS 16 | DN 400 | 1410 mm | ~3200 kg |
Service fit
Where this valve is used
Typical applications
- Main steam and reheat on supercritical and ultra-supercritical units
- High-pressure feedwater on plants that two-shift
- Hydrocracking and high-pressure hydrogen service
- Coal gasification and IGCC
- Any duty where thermal fatigue rather than static pressure governs
Selection limits to check
- Throttling. The forging route does not change what a partly open wedge does to a seat.
- Sizes above the available press and handling capacity, where a sound casting is the sensible route. The crossover size is stated per item rather than as a general claim.
- Short lead times. Forged billets in creep grades have real procurement time and it is quoted honestly.
- Budget-driven substitution. If a cast body is adequate for the duty we will say so rather than sell the more expensive route.
Quality assurance
Inspection & delivery documents
The inspection and test plan defines the agreed scope, hold points and witness points for your order.
Inspection scope
- Hydrostatic shell test to API 598 / MSS SP-61
- Hydrostatic or pneumatic seat test, leakage rate per specification
- Back seat test (gate and globe, where a back seat is supplied)
- PMI on all pressure-containing parts and welded overlays
- NDE per specification - RT, UT, MT or PT as applicable
- Hardness survey after post-weld heat treatment
- Dimensional inspection against approved GA drawing
- Material certification EN 10204 3.1 (3.2 on request)
- Visual and functional check, full stroke on the manual operator
Document package
- Product datasheet
- General arrangement (GA) drawing
- Inspection & Test Plan (ITP)
- Material test certificate (MTC) EN 10204 3.1
- Hydrostatic and seat test report
- PMI report
- NDE reports as applicable
- Heat treatment charts
- Dimensional report
- Packing list and preservation record
Reference framework
Applicable standards
Pressure-temperature ratings, materials, wall thickness, testing and marking. This is the base rating standard for the valve - it is what fixes the allowable pressure at your design temperature.
Face-to-face and end-to-end dimensions. Relevant when the valve replaces an existing one or has to drop into a fixed spool.
Butt welding end preparation, including bore and bevel geometry for the matching pipe schedule.
Inspection and pressure testing - which tests are mandatory, test durations and allowable leakage. We state the shell and seat test scheme on the ITP.
Alternative pressure testing scheme for steel valves, used where the project specification calls for it instead of API 598.
Marking of the body and the nameplate - size, class, material heat, figure number and flow direction where applicable.
Buying questions
Frequently asked questions
How do I verify the body is genuinely one-piece forged?
Ask for the general arrangement drawing and the forging drawing rather than the brochure. The GA shows whether the neck is part of the body. Then check the ITP: a one-piece forged body has no body weld, so a body weld line on the ITP tells you what you are actually being supplied.
Is forged always better than cast here?
Against porosity, through-thickness properties and thermal fatigue, yes. Against cost, lead time and shape freedom, no. On a base-load unit at moderate class a sound cast body is entirely appropriate, and we will tell you when that is the case.
What is the difference between integral forged and one-piece forged?
They are used loosely across this industry and they are not interchangeable on every valve. We apply one test and state it per item: whether the pressure-containing body including the neck came from a single forged piece. Anything else is described as what it is.